 English
 русский
Direct gate of plastic injection mold runner system design
In order to get the best injection quality, the gate type must be selected carefully, the coommon gate tyeps are: direct gate, side gate, pin-point gate, sub gate,valve gate of hot runner etc. Among them, the side gate is divided into tab gate, ear protection gate, fan gate, thin gate and so on, the sub gate is divided into sub gate, banana gate, downturning gate and so on.
According to the production automation, it is divided into manual removal and automatic removal, the side gate and direct gate are need to be manually removed after production,but the sub gate and pin-point gate and valve gate of hot runner are automatic removed, we wil dicuss the direct gate today:
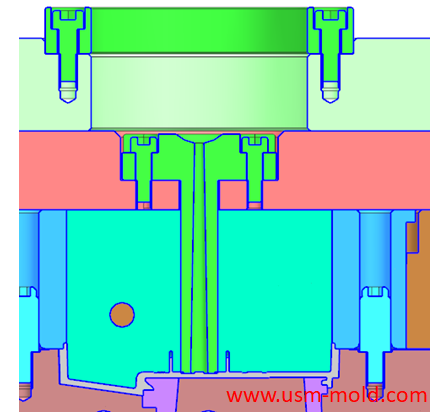
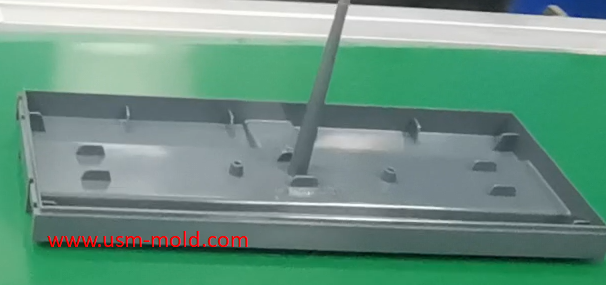
Direct gate (Sprue gate): direct gate is also called main runner type, the plastic enters the cavity directly through the main runner, as shown in picture 1a and picturee 1b.
Picture 1a
Picture 1b
Advantage:
1. The product size is accurate and the molding quality is good, due to the gate size is big which is less affected by other external factors, so the part size of is better controlled during injection molding, and the injection molding process range is also big;
2. Saving runner processing, the direct gate is usually the gate sleeve that directly enters the product (as shown in picture 1a), and the direct gateh is a standard part, which is already processed after buying it, and there is no need to process the main runner and sub runner on the mold core etc.;
3. Less pressure loss, the direct gate size is generally big, and it is directly injected into the product from the nozzle of the injection molding machine, without the conversion between the main runner and the sub runner, so the process is shorter and the injection pressure loss will be relatively small;
4. Products with large or depth can be formed, because the gate size is bigger than that of the general gate, the flow length ratio of the product will be longer, and the molded product will have an advantage, because the product is directly docked by the nozzle of the injection molding machine, and the nozzle of the injection molding machine may be prolong, so it has obvious advantages when injecting deeper products;
5. It is conducive to hold pressure (feeding shrinkage), because the direct gate size is big and the process is short, the pressure in the pressure holding stage of the injection molding process is relatively small, which is very obvious to solve the issue of product shrinkage;
6. Conducive to product exhaust, this type of gate is generally located in the center of the product, and the molten plastic during injection is diffused and filled from the middle to the surroundings, so the air trapping problem of the product is very easy to solve.
Disadvantages:
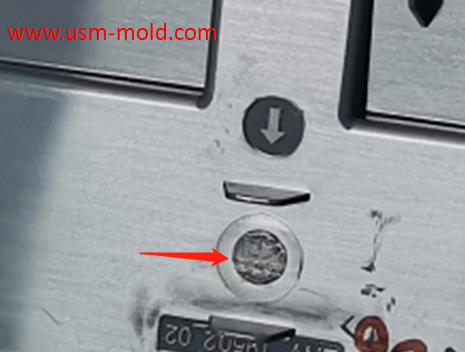
1. Gate marks will affect the appearance, because this gate is generally designed in the center of the product, there will be a mark after cutting the gate (as shown in picture 2), which is not suitable for products with high appearance requirements;
2. Flat and shallow products are prone to warpage and deformation, because this type of gate is generally in the center of the product, the pressure in the middle of the product is the largest during injection molding, and the pressure around it will be much less. Therefore, after the product pick up of the mold, due to the stress formed by the pressure difference, the product is easily warped deformation
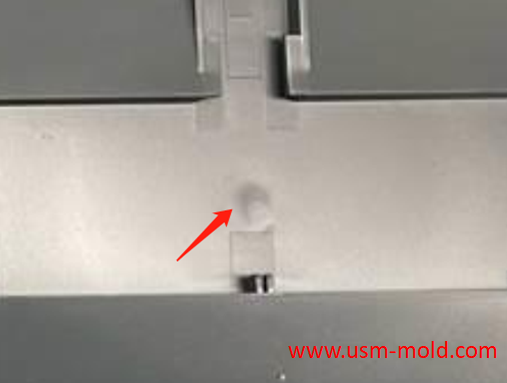
3. The stress mark is big, the stress at the gate is also big, and stress marks will be formed on the back of the product (as shown in Figure 3), which will affect the appearance of the product.
4. Only one product can be formed at one time, because the center of the nozzle of the injection molding machine is facing the part gate, there is no conversion between the main runner and the sub runner, so only one product can be molded at a time.
We will share the side gate of the plastic mold gating system design in following news.
Plastic injection mold runner system design
Jan 16, 2022The gate is the connecting part between the runner and the cavity, and is also the end part of the injection mold gating system, the molten plastic enters the cavity and core side through the gate...view
Key points of gas-assisted injection molding process
Apr 20, 2022Gas injection parameters The gas-assisted control part is a device that controls the gas pressure in each stage, the gas-assisted parameters have only two values: gas injection time (seconds) and gas...view
Parting surface venting of runner system
Mar 10, 2022There are a large amount of gas in the main and sub channel, these gas are discharged through the pull rod (push rod) during injection processing, a part of gas come out from exhaust slot on parting...view
Plastic part ribs desigining
Jan 4, 2022The ribs function: The role of ribs is to improve the strength and rigidity of the plastic parts, prevent the plastic parts from being distorted and deformed, and will not cause the appearance of the...view
Insert pin of vengting design for molded parts
Mar 20, 2022Insert pin of venting: It is difficult to make exhaust slot when end runner is not in parting surface during injection, and there is no matching gap available, but we could make the venting pin at end...view
Reasons for making the exhaust system of the injection mold
Feb 28, 2022The gas in the injection mold includes not only the air in the cavity, but also the air in the gate and the decomposition gas generated by the plastic melt, and the steam which caused by plastic in...view