 English
 русский
The main reasons for air trapping of plastic injecton mold
During the injection molding process, the front end of the slight ribs may be air trapped and plastic burnt, and also cause the molded part may become black and carbonized.
The mechanism of air trapped scorching is that when the air in the mold cavity is extruded by the molten plastic flowing into the cavity, the air will heat due to being compressed if it is in a sealing state without an outlet, and then it leads to combustion and burns.

Since the air is a kind of gas, it can be compressed, but it generates heat when compressed, it is like when we use a pump to inflate our bike tires, the pump gets hot.
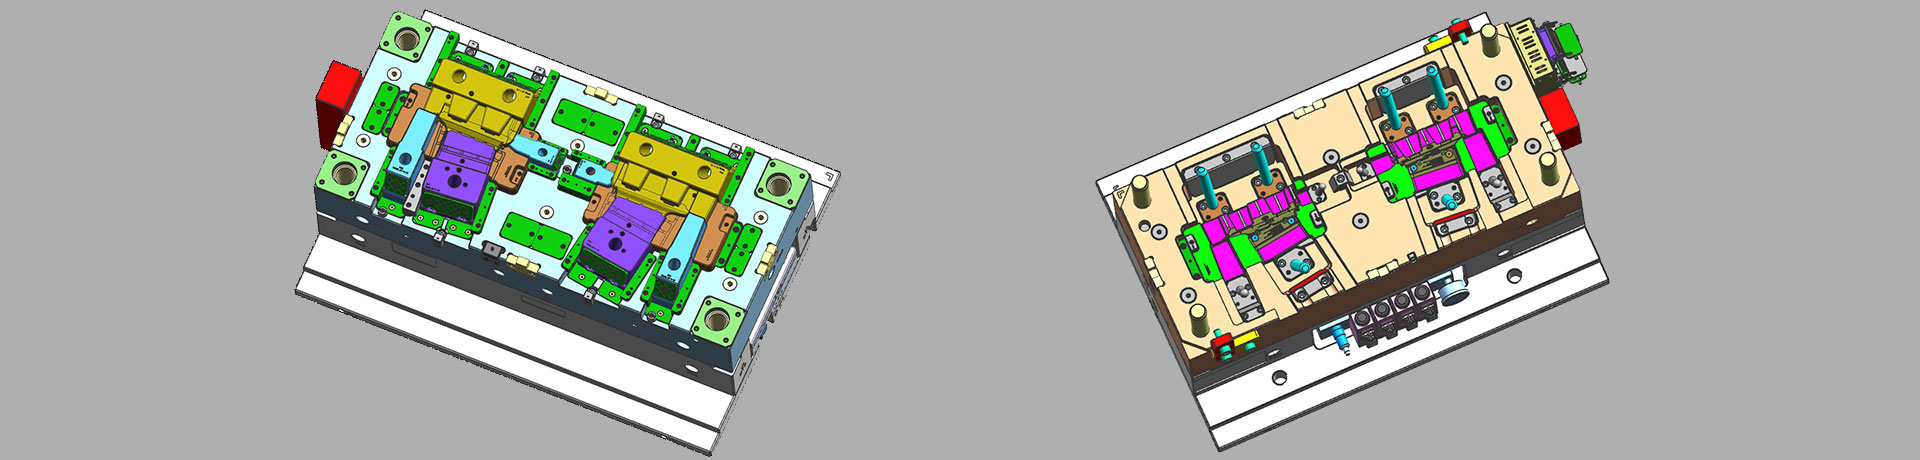
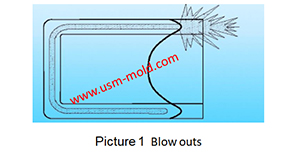
The compression of the residual air in the cavity usually occurs in a short time of about 0.1 to 0.5 seconds, because it is compressed under a high pressure of 200 to 500 kgf per square centimeter, it is easy to heat up to the ignition point of the plastic (as shown in picture 1).
Therefore, for some slight ribs, pillars and other product features in the gas injection mold, it is necessary to make venting slot to let the gas in the mold which can be discharged to the outside of the cavity.
Gas-assisted injection molding product defects and solutions
Apr 28, 2022Common defects and solutions of gas-assisted injection moulding: 1. Gas blows out the melt like in picture 1. Reason: insufficient pre-filled amount. When the plastic part is a locally thickened...view
USM Blogo Opening
Oct 27, 2021Hello everyone! Our blog is open today, it is very glad to have the opportunity to meet you here, welcome to visit us whenever you need. USM is a professional plastic injection mold and molding...view
Design standard of exhaust slot
Mar 3, 2022The exhaust system should ensure that the gas in the cavity is smoothly discharged, and also prevent the material from entering and exhausting channels from causing flashing of the product or blockage...view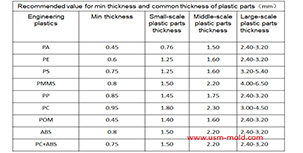
Design principles for wall thickness of plastic products
Jan 3, 2022The principles of wall thickness design for plastic parts are as follows: 1. Making the wall thickness even is the first principle of plastic part design, it can make filling, cooling and shrinking...view
Plastic molding shrinkage rate
Dec 30, 2021Plastic parts getting smaller by shrink, due to the temperature decrease during the molding process, and the shrinkage is expressed by the shrinkage rate, it is common plastic shrinkage rates are...view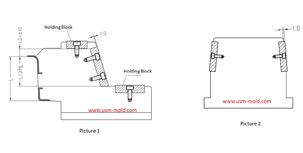
The design requirements of slider wear plate
Jan 2, 20241. The wear plate of slider requires hardening treatment, with a hardness of 45-48HRC; 2. The friction surface of the wear plate is required to be 1.0mm higher than the slider surface (see picture-1);...view