 English
 русский
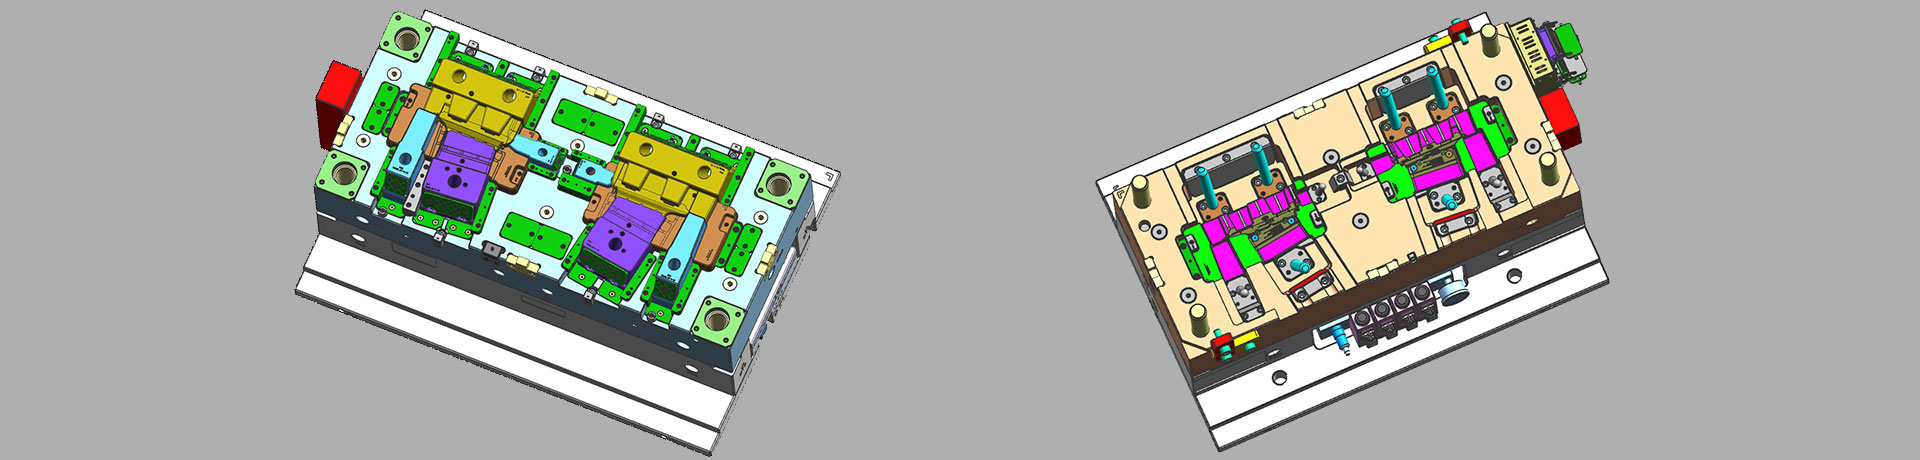
Slider designing tips 2
9. The molding parting surface of the slider molding should be made as a shut-off surface as possible, and the width of the shut-off part should be at least 8mm, and do not make a shut-off surface;
10. When using the center guide slider, we should follow the company standard "slide center guide slider design" strictly;
11. When the mold is closed, if there is a risk of interference between the slider and other parts, the reset mechanism must be done first;
12. The core-pulling distance of the slider must be bigger than the actual core-pulling distance of the product by 3-5mm;
13. The large slider should be avoided to be set in the direction of the top side of the mold as far as possible; if it is unavoidable, it should be driven by an hydralic cylinder, and a stroke switch should be installed to cooperate with it;
14. When the cylinder core-pulling device is not used for the slider on the day side, the strength of the slider limit device must be checked to ensure that the weight of the slider does not exceed 2/3 of the strength of the limit device to prevent accidents;
15. When the slider is set on the ground side, the spring can be cancelled, but at the same time, a reliable stop should be designed to prevent the slider from falling off due to its own weight;
16. The same material cannot be used if there is frictional movement between the parts or the requirements of the insertion.
Venting system of plastic injection mold introduction
Feb 27, 2022Hello everyone, thanks for attention. We’ve discussed about the temperature control system earlier, now we are going to talk about the mold venting information in following 11 articles, from the...view
Controling method of plastic injection mold temperature
Feb 15, 2022Except for heat radiation and heat convection from the mold, most of the heat bring into the mold by the plastic needs to be taken out of the mold by the circulating heat transfer medium by heat...view
The difference between full shot and short shot of gas-assisted injection molding
Apr 13, 2022Gas-assisted injection molding can be divided into short shot and full shot. Short shot The short shot method is shown in picture 1, it is suitable for thick-walled plastic parts with low mold filling...view
Gas-assisted injection molding product defects and solutions
Apr 28, 2022Common defects and solutions of gas-assisted injection moulding: 1. Gas blows out the melt like in picture 1. Reason: insufficient pre-filled amount. When the plastic part is a locally thickened...view
The T slot of slider and guider designing tips
Dec 18, 20231. The T slot of slot should be designed according to the picture 1, If there is a relatively high slider, the slider T slot is not high enough which will cause the center of gravity to be unstable,...view
Key points of gas-assisted injection molding process
Apr 20, 2022Gas injection parameters The gas-assisted control part is a device that controls the gas pressure in each stage, the gas-assisted parameters have only two values: gas injection time (seconds) and gas...view