 English
 русский
Reasons for making the exhaust system of the injection mold
The gas in the injection mold includes not only the air in the cavity, but also the air in the gate and the decomposition gas generated by the plastic melt, and the steam which caused by plastic in high temperatures. During injection molding, these gases should be exhaust in time, otherwise there will be some issues as following:
1. Defects such as flow mark, water mark, and weld marks will be formed on part surface;
2. Defects such as bubbles and loose tissues inside the plastic parts, which will lead to insufficient filling inside plastic part;
3. It is difficult to fill the plastic melt or flash locally;
4. The gas generates high temperature under high temperature and high pressure, causing local carbonization and burnt marks on the product;
5. Reducing the filling speed of the plastic melt, not only the molding cycle is prolonged, but the melt temperature decreases quickly after injection speed dropped, the residual stress will increase, if the injection pressure is increased, and the possibility of warping deformation of the plastic part after demolding will increase, if the material temperature is increased in order to reduce the injection pressure, it will cause the plastic to crack.
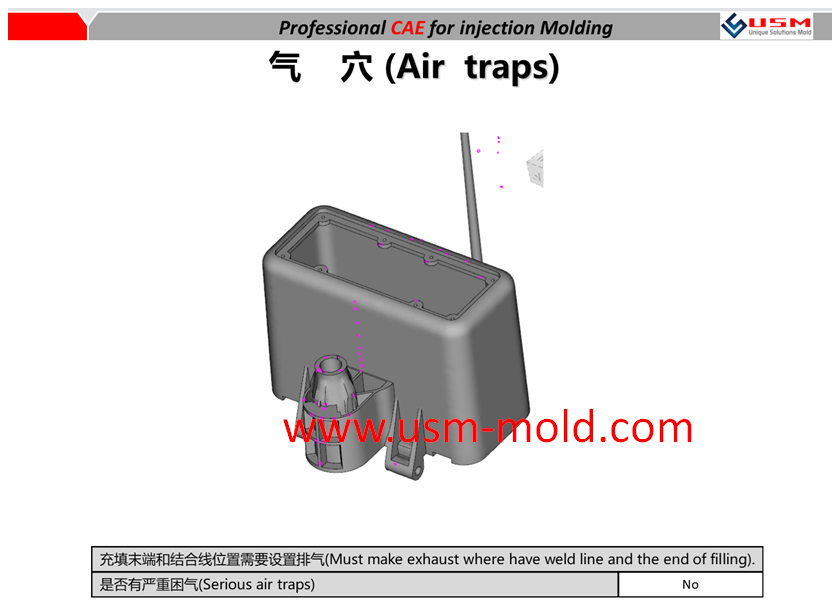
Properly making the exhaust slot can reduce the injection pressure greatly, reduce the injection and the holding time, and reduce the clamping pressure, thereby improving the production efficiency, reducing the production cost, and the energy consumption of the machine. For transparent plastic parts or plastic parts with strict surface requirements, we should be careful with the mold exhaust system design.

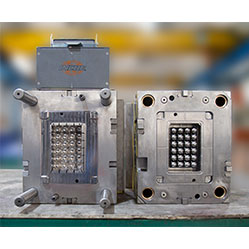
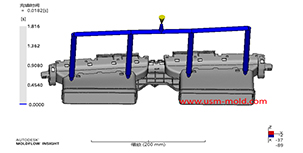
Plastic injection mold runner system design points
Jan 9, 2022When designing the gating system, Firstly, we should consider making the plastic melt fill the cavity with core side quickly to reduce pressure and heat loss; secondly, it should be economically...view
Key points of plastic injection mold runner system
Jan 12, 2022The sub-runner is a transitional channel between the main runner and the gate, as the sub-runner is the longgest part of gating system, so it is very important to enhance the parts quality and improve...view
Design principle of plastic injection mold cooling system
Feb 13, 2022Design principle of cooling system In order to improve the efficiency of the cooling system and make the cavity surface temperature distribution even, the following principles should be followed in...view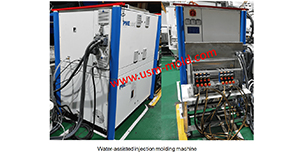
Water assisted injection molding introduction
May 11, 2022Like the gas-assisted injection molding process, water-assisted injection molding injects a piece of plastic into the mold cavity and core firstly, and then injects water to squeeze the melt plastic...view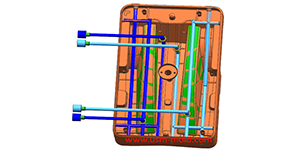
The principle of mold temperature balance in plastic mold cooling system design
Feb 21, 2022The principle of mold temperature balance: 1. Due to the complexity of the plastic parts and mold structure, it is difficult to make the temperature of the mold completely consistent, but should be...view
Comparison of water-assisted and gas-assisted injection molding
May 19, 2022Comparing with water-assisted injection molding technology and gas-assisted injection molding technology, the fundamental difference is the nature of the auxiliary molding media used. One is liquid...view