 English
 русский
Slider designing tips 1
1. After the slider core pulls out, the length of staying in the guide pin slot should not be less than 2/3 of the total length of the slider, for special cases, the slider slot can be partially lengthened;
2. In principle, the length of the sliding part of the slider should be bigger than 1.5 times the height of the slider;
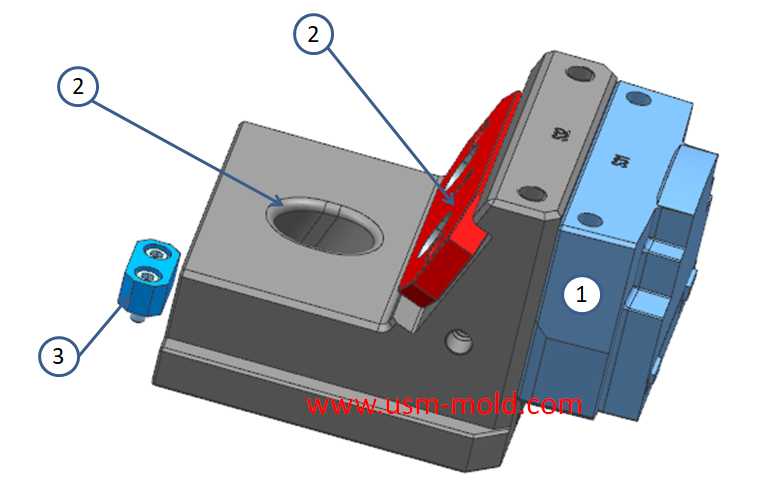
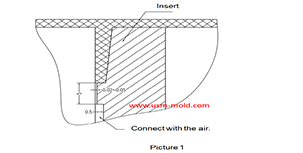
3. The mating surface of the cross-section surface of the slider going deep into the fixed die is made into a side slope of 3~5° to avoid air or unilateral, as shown in 1 in picture 1;
4. The maximum angle of the angle pin shall not exceed 22°,, and the wedge angle of the slider is 2-3° larger than that of the angle pin;
5. The entrance of the angle pin hole of the slider should be made into an R angle, as shown in 2 in picture 1;
6. The matching gap between the angle pin hole of the slider and the angle pin should be avoided by 0.5-1.0mm on one side;
7. After the slider is pulled out, there must be a stroke switch, and the slider limit device with a compression spring and a stop is preferred, as shown in 3 in picture 1;
8. A wear plate is required for the locking part of the slider, as shown in 4 in picture 1, the slider and the top of the entrance of the locking block make an R angle.
Venting insert design of molded parts
Mar 13, 2022In the thin-walled cavity, the end of the melt flow, the bottom of the blind hole of the mold cavity, the end of the solid column of the plastic part, the bottom of the plastic part rib and screw...view
Gate position determination of plastic injection mold runner design system
Jan 17, 2022In the selection of gate location, the following issues should be paid attention to: 1. The gate position should be set at the maximum wall thickness of the plastic part, so that the plastic melt...view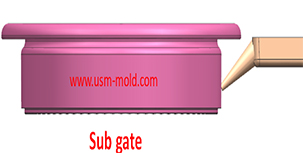
The sub gate of the plastic injection mold runner system
Jan 26, 2022In order to get the best injection quality, the gate type must be selected carefully, the coommon gate tyeps are: direct gate, side gate, pin-point gate, sub gate,valve gate of hot runner etc. Among...view
Different treatment of plastic injection mold cooling system principles
Feb 22, 2022Different treatment principle: 1. The mold temperature is different according to the different plastics, when the plastic requires the molding temperature of the mold to be ≥80°C, the mold must be...view
What is Plastic Injection Mold?
Dec 27, 2021The plastic mold is used for injection molding, it is assembled with cavity, core and side slider together, with ejection system and adjustments to produce plastic products by different shapes and...view
Plastic injection mold runner system design
Jan 16, 2022The gate is the connecting part between the runner and the cavity, and is also the end part of the injection mold gating system, the molten plastic enters the cavity and core side through the gate...view