 English
 русский
TV bracket mold supplier
 Design & EngineeringWe always insist that Design & Engineering is the core for mold, the USM engineering team will maintain communication closely with our customers at any time, from a project starting, they will participate in the customer's product design together.More+
 Five Major Steps of the Injection Mold Production ProcessInjection mold manufacturing can be roughly divided into the following steps:Process analysis of plastic products.More+
 Automotive Grille MoldThe part surface of the air intake grille generally has several treatment methods such as leather texture, sandblasting, paint spraying, and electroplating, the materials usually are PP, ABS, ASA, etc., and the surface of the bumper decorative grille is generally treated with leather texture and sandblasting, mainly PP material.More+
 Medical Mold Injection ProductMedical devices have strict standards for molds, mainly involved in mold design, mold steel, manufacturing accuracy, sanitary production conditions, and transportation condition and many other aspects.More+

 Injection MoldingUSM is a professional one-stop service for plastic injection molding companies in China, with our rich experience by mold-making capabilities, we ensure that mass products can be manufactured in the shortest time.More+
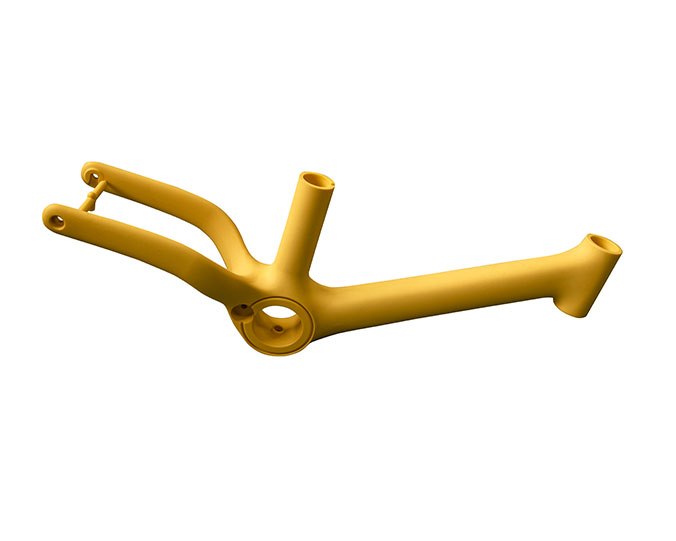 Gas & Water Assisted Injection MoldThe differences between water-assisted and gas-assisted molding1. Water-assisted injection molding uses water, and it can be recycled and reused, so the medium water of the two molding processes is cheaper than nitrogen.More+
_20250317101516A021.jpg) The basic points of designing gas-assisted injection molding1. Firstly, considering the suitable wall thickness areas needs to be injected and hollowed out, and then decide how to connect them with the gas channel;2. The gas channel should be arranged in balan...More+
 Parting surface venting of runner systemThere are a large amount of gas in the main and sub channel, these gas are discharged through the pull rod (push rod) during injection processing, a part of gas come out from exhaust slot on parting s...More+
 Automotive Mold SupplierWith over 15 years of experience in automotive mold development and production, USM will make mold flow analysis from the DFM report step to ensure that the pressure will be controlled at a reasonable range during injection, and there are no weld marks and other defects on the part surface.More+
- Parting surface venting of runner systemThere are a large amount of gas in the main and sub channel, these gas are discharged through the pull rod (push rod) during injection processing, a part of gas come out from exhaust slot on parting s...More+
 Multi Cavity Medical MoldMedical equipment products are divided into many different types, some products do not contact the human body, some contact the human body, some enter the body, and some products need to pass the FDA Alcohol test, some have to pass the FDA n-ethane test.More+
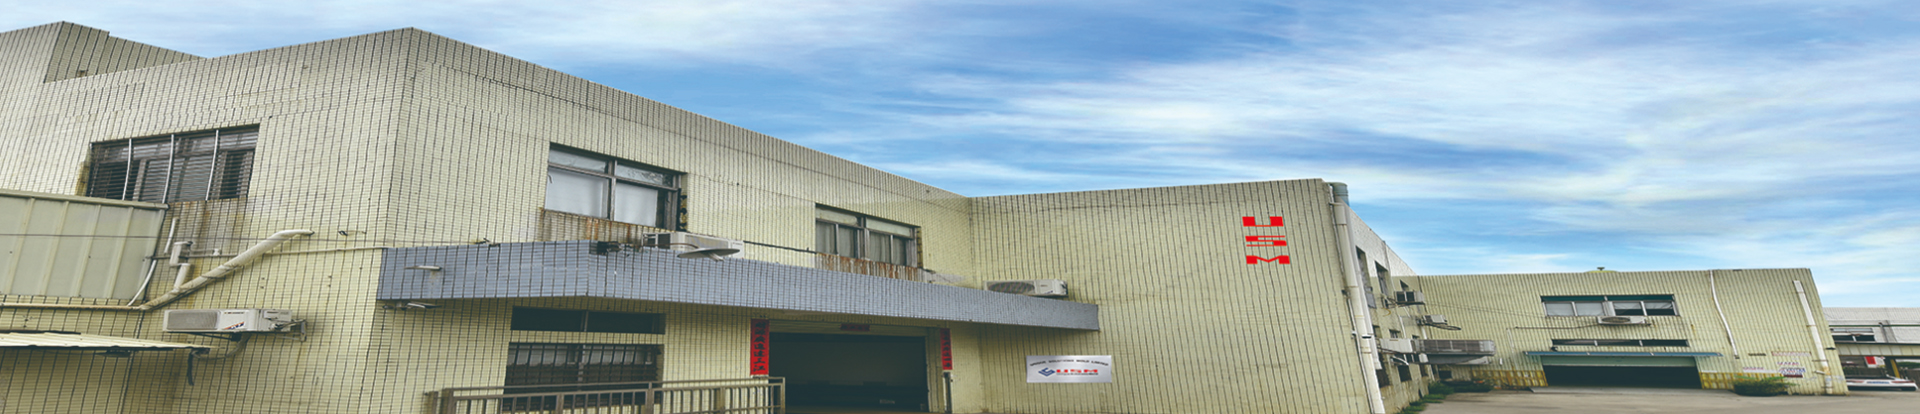 Company ProfileUSM is one of the world's leading manufacturers of the plastic injection mould and molded parts. We have always pushed developments forward and set benchmarks in Automotive, High precision, and 2K...More+
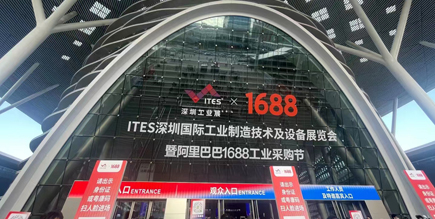 2022 Shenzhen Industrial Exhibition ITES ended successfullyThe 2022 ITES Shenzhen International Industrial Manufacturing Technology and Equipment Exhibition and the 23rd Shenzhen International Machinery Manufacturing Exhibition were grandly opened in Shenzhen...More+
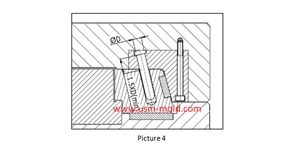 The common fixing method of angle pinThe angle pin is a common part of the drive slider, and the fixing and installation methods as following:1. Pass through the mold plate directly and press the angle pin with the top plate to fix it, a...More+
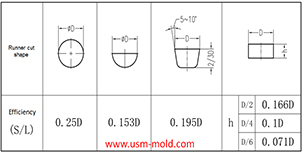 Hydraulic diameter conversion of runners in plastic mold gating system designHydraulic diameter refers to 4 times the ratio of the flow cross-sectional area to the perimeter, as the wall shear stress of non-circular pipes is not even distributed along the surrounding walls, on...More+
_20250317101937A023.jpg) What is the side parting and core pulling mechanisms with their function?When there are holes, cavities or cores on the inside or outside of the injection-molded plastic parts that are different from the opening and closing directions of the mold, the plastic parts cannot...More+
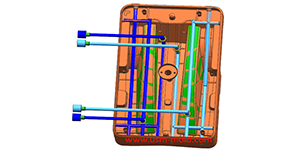 The principle of mold temperature balance in plastic mold cooling system designThe principle of mold temperature balance:1. Due to the complexity of the plastic parts and mold structure, it is difficult to make the temperature of the mold completely consistent, but should be mak...More+
 New Five-axis CNC Machine ArrivalThe new 5 axis CNC machining machine has arrived in our workshop on 6th Nov. 2021 and is now putting into use.GMU-6350 type CNC machining machineWorking stroke (XYZ): 630*500*550Maximum loading: 800kg...More+
 PLC Controller Shell MoldMore and more people will have a high standard for a better life, most of home appliance product surfaces were made by mirror polishing, it requires for high standard to mold steel and polishing way, good mold steel without a technical polishing engineer, the product can not reach the high standard, they always work together.More+
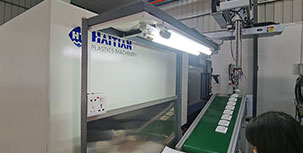 What is Ejection Molding?The process to get injection molded products is called injection molding, or called injection. Injection molding is an important method in polymer molding processing, it is characterized by a short molding cycle and high production efficiency.More+
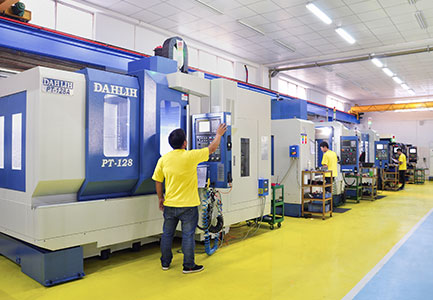 Mold ManufacturingUSM is a one-stop service for plastic precision mold and injection molding factory in China, as we know, perfect molds are related to professional mold design, high precision processing machines, rich experiences assembling workers, and team management.More+
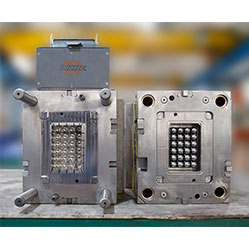 Medical Plastic MoldProduct material: PP material in medical-gradeMold steel: S136 HRC 52-54Mold life: 1 millionHot runner brand: IncoeMold base: LKMSurface finishing: Mirror polishingMold lead time: 6 weeksMore+
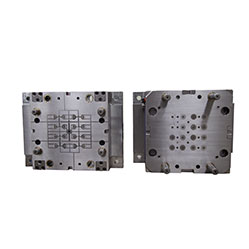 16 Cavities Plastic Injection MoldA 16-cavity multi cavity mold means that 16 pieces of parts can be produced in one injection cycle at the same time, which can improve the production efficiency greatly, save production time and reduce production cost.More+
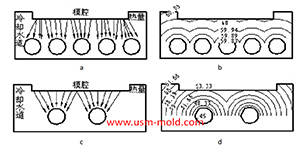 Factors affecting the cooling rate of parts by injection moldingIt should be shaped by cooling to get stable plastic part after plastic filling the cavity and core side, so most injection molds need to be equipped with cooling devices to make the mold temperature ...More+
 USM Blogo OpeningHello everyone! Our blog is open today, it is very glad to have the opportunity to meet you here, welcome to visit us whenever you need.More+
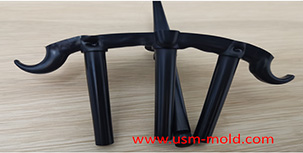 Banana gate of plastic injection mold runner system designIn order to get the best injection quality, the gate type must be selected carefully, the coommon gate tyeps are: direct gate, side gate, pin-point gate, sub gate,valve gate of hot runner etc. Among ...More+
- Gas & Water Assisted Injection MoldThe differences between water-assisted and gas-assisted molding1. Water-assisted injection molding uses water, and it can be recycled and reused, so the medium water of the two molding processes is cheaper than nitrogen.More+
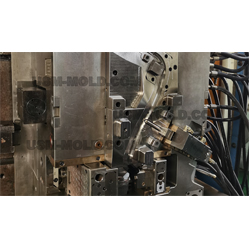 Engine Coolant PipeIn the gas-assisted injection molding process, the gas always follows the path with the least flow resistance, from high pressure to low pressure, and flows to the thick wall part, because the temperature of this part is high and the resistance is small.More+
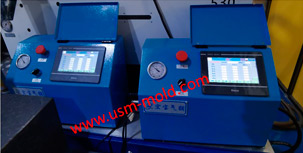 Gas-assisted Injection Molding EquipmentThe gas-assisted equipment includes a gas-assisted control part and a nitrogen generator, it is special and seperate system of the injection molding machine, and its only interface with the injection ...More+
- Multi Cavity Medical MoldMedical equipment products are divided into many different types, some products do not contact the human body, some contact the human body, some enter the body, and some products need to pass the FDA Alcohol test, some have to pass the FDA n-ethane test.More+
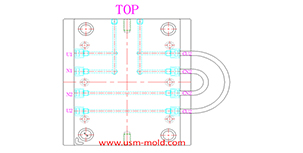 Different treatment of plastic injection mold cooling system principlesDifferent treatment principle:1. The mold temperature is different according to the different plastics, when the plastic requires the molding temperature of the mold to be ≥80°C, the mold must be he...More+
- Automotive Grille MoldThe part surface of the air intake grille generally has several treatment methods such as leather texture, sandblasting, paint spraying, and electroplating, the materials usually are PP, ABS, ASA, etc., and the surface of the bumper decorative grille is generally treated with leather texture and sandblasting, mainly PP material.More+
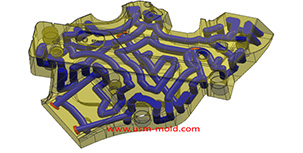 Plastic cooling factors by injection parameter1. Plastic parts design: mainly for the wall thickness of plastic products. The thicker thickness of the product, the longer the cooling time. Generally speaking, the cooling time is approximately pro...More+
 Amazing Outdoor TravelingOur team experienced wonderful outdoor walking a few weeks ago. we took a big bus from our office to the destination which is very natural and frosty with a very clean river dotted with cobblestones. we walked through the small rivers by naked feet.More+
- Plastic Box MouldThe operation way of smart home appliances is very diversified, It can be operated with a smart touch screen, a scene remote control, a mobile phone, or a computer. There is no limitation for time and place which can be operated at any time and any place, any devices realize intelligent control.More+
 Air Chamber MoldWith over 15 years of pre-deformed mold, USM Mold has mastered scientific and complete pre-deformation mold technology, from project management, mold flow analysis, design, manufacturing, assembling, mold trial, and final measurement.More+
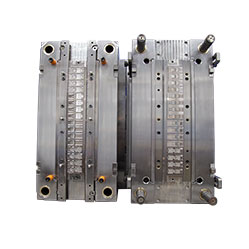 Metal Insert MoldFor rigid molded parts and curved elastic molded products on rubber gaskets, after injection molding on the substrate, an integrated product can be made, and the complicated operation of arranging the sealing ring can be omitted, making the automatic combination of the subsequent processes easier. Because it is the joining of the molten material and the metal insert, compared with the press-in molding method, the gap of the metal insert can be designed to be narrower, and the reliability of composite product molding is higher.More+
_20250317101606A022.jpg) Several common process of water-assisted injection molding introductionAccording to the design of the injection molding machine and the casting system, the corresponding melt-returning process of water-assisted injection molding can be roughly divided into two types: the...More+

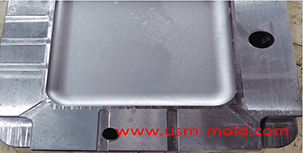 Venting system of plastic injection mold introductionHello everyone, thanks for attention. We’ve discussed about the temperature control system earlier, now we are going to talk about the mold venting information in following 11 articles, from the reas...More+
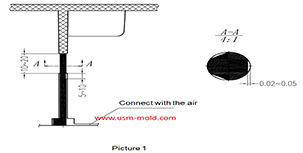 Insert pin of vengting design for molded partsInsert pin of venting:It is difficult to make exhaust slot when end runner is not in parting surface during injection, and there is no matching gap available, but we could make the venting pin at end ...More+
- What is Ejection Molding?The process to get injection molded products is called injection molding, or called injection. Injection molding is an important method in polymer molding processing, it is characterized by a short molding cycle and high production efficiency.More+
- Voice Operated Switch MoldWe know that the basic goal of smart home appliances is to provide people with a comfortable, safe, convenient and efficient living environment. Therefore, the most important thing for smart home appliance products is to take practicality as the core, remove those flashy functions, and use practicality, ease of use, and humanization.More+
- 2022 Shenzhen Industrial Exhibition ITES ended successfullyThe 2022 ITES Shenzhen International Industrial Manufacturing Technology and Equipment Exhibition and the 23rd Shenzhen International Machinery Manufacturing Exhibition were grandly opened in Shenzhen...More+
- The common fixing method of angle pinThe angle pin is a common part of the drive slider, and the fixing and installation methods as following:1. Pass through the mold plate directly and press the angle pin with the top plate to fix it, a...More+
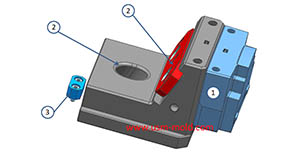 Slider designing tips 11. After the slider core pulls out, the length of staying in the guide pin slot should not be less than 2/3 of the total length of the slider, for special cases, the slider slot can be partially lengt...More+
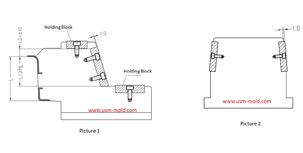 The design requirements of slider wear plate1. The wear plate of slider requires hardening treatment, with a hardness of 45-48HRC;2. The friction surface of the wear plate is required to be 1.0mm higher than the slider surface (see picture-1);3...More+
- Medical Plastic MoldProduct material: PP material in medical-gradeMold steel: S136 HRC 52-54Mold life: 1 millionHot runner brand: IncoeMold base: LKMSurface finishing: Mirror polishingMold lead time: 6 weeksMore+
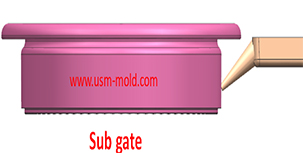 The sub gate of the plastic injection mold runner systemIn order to get the best injection quality, the gate type must be selected carefully, the coommon gate tyeps are: direct gate, side gate, pin-point gate, sub gate,valve gate of hot runner etc. Among...More+
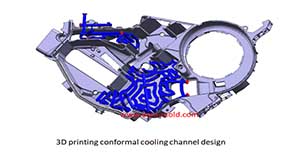 Controling method of plastic injection mold temperatureExcept for heat radiation and heat convection from the mold, most of the heat bring into the mold by the plastic needs to be taken out of the mold by the circulating heat transfer medium by heat condu...More+
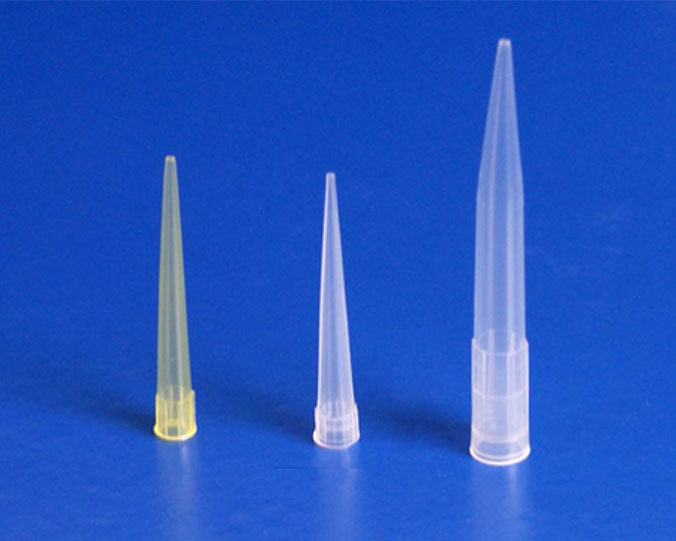 Medical Plastic Injection MoldWhat is the medical injection molded parts?For medical plastic manufacturers, it means that medical supervisors are required to supervise and manage the materials used to manufacture the equipment.More+
- Air Chamber MoldWith over 15 years of pre-deformed mold, USM Mold has mastered scientific and complete pre-deformation mold technology, from project management, mold flow analysis, design, manufacturing, assembling, mold trial, and final measurement.More+
- Slider designing tips 11. After the slider core pulls out, the length of staying in the guide pin slot should not be less than 2/3 of the total length of the slider, for special cases, the slider slot can be partially lengt...More+
- Water Proof Plastic Enclosure MoldThe product will be made by two times, which will inject the second piece after finishing the first piece in the other mold and different injection machine, normally will be no specific request for 2 different pieces injection time, injection machine.More+
 PA66 GF30 Car Parts Plastic Injection MoldPre-deformation means that the product will be designed mold in opposite direction in advance. The product is injected and cooled by natural shrinkage, the two deformations will be offset to obtain a product and meet the drafting tolerance.More+
 Bike Frame Mold for KidsDuring plastic molding processing, gas-assisted injection molding is abbreviated as GAIM, which is a relatively new molding processing technology, this technology is comprehensively developed on the basis of the design and manufacture of traditional injection molding molds and blow molding molds, and entered the practical stage in the 1990s, gas-assisted injection molding has huge technical application advantages and can produce significant economic benefits.More+
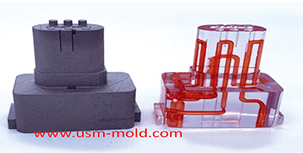 Conformal cooing channel of plastic injection moldThe conformal cooling gate is a new type of mold cooling gate based on 3D printing technolog, because of its processing characteristics, the conformal cooling gate can fit the shape of the product wel...More+

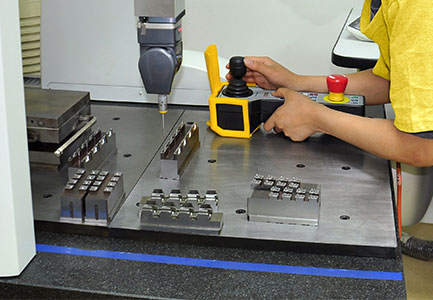 Quality ControlQuality is the soul of USM at all times, the procedure of quality control, quality insurance, and quality monitoring are integrated into every operation step, and all operations are guaranteed with ISO 90001.More+
- USM makes a good job in mould industryProject management, manufacturing and engineering capabilities including project managerment solution, production design, development, mould and prototyping, material selection, manufacturingMore+
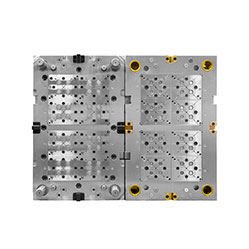 32 Cavity MoldUSM has many years of experience in the design and manufacturing of multi-cavity molds and is particularly good at fast-selling products in medical and daily consumer products.More+
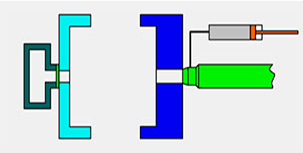 The difference between full shot and short shot of gas-assisted injection moldingGas-assisted injection molding can be divided into short shot and full shot.Short shot The short shot method is shown in picture 1, it is suitable for thick-walled plastic parts with low mold filli...More+
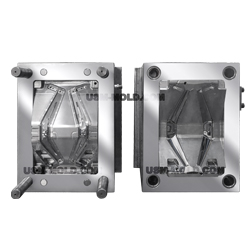 TV Frame MoldPushing the liquid plastic into the cavity and core side by high pressure during the injection process, and the gas pressure is maintained to form a hollow section inside the thick wall of the plastic part, the injection process is called gas-assisted injection molding.More+
- Gas-assisted Injection Molding EquipmentThe gas-assisted equipment includes a gas-assisted control part and a nitrogen generator, it is special and seperate system of the injection molding machine, and its only interface with the injection ...More+
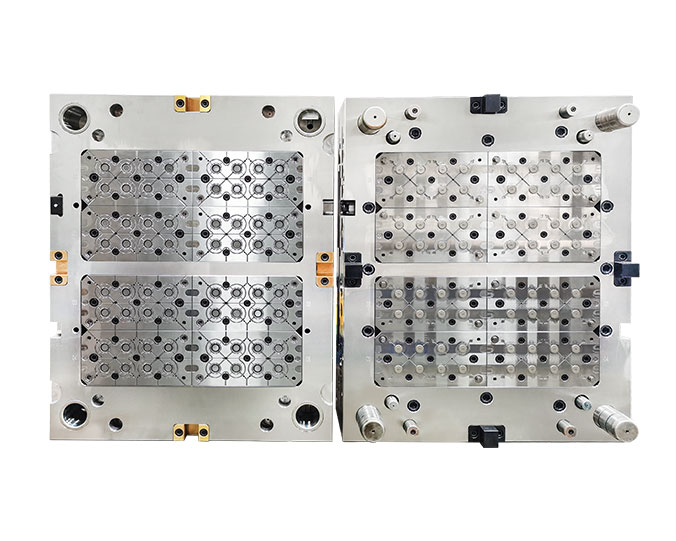 Multi Cavity MoldMulti cavity mold requires very high machining accuracy. if the machining error of one single cavity is 0.01mm, and the total tolerance of 64-cavity processing will be very big. therefore, to make the multi-cavity mold request very advanced processing equipment in order to ensure the machining accuracy.More+
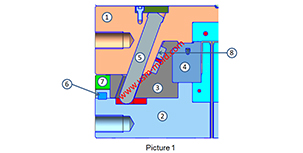 Slider of side core pulling mechanisum assemblingThe picture 1 shows a typical guide pin driven slider parting and core-pulling mechanism, we will talk about the composition and function of the lateral core-pulling mechanism.1. Lateral forming parts...More+
- The difference between full shot and short shot of gas-assisted injection moldingGas-assisted injection molding can be divided into short shot and full shot.Short shot The short shot method is shown in picture 1, it is suitable for thick-walled plastic parts with low mold filli...More+
 Automotive Fan MouldThe common products used to be water chambers, air chambers, engine inlet valve pipe and nylon connectors, and automotive AC systems: fan covers, fans, automotive brackets, sunroofs, mirror triangle brackets, automotive bottom sheets, and so on.More+
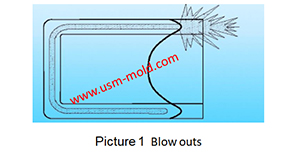 Gas-assisted injection molding product defects and solutionsCommon defects and solutions of gas-assisted injection moulding:1. Gas blows out the melt like in picture 1. Reason: insufficient pre-filled amount. When the plastic part is a locally thickened plate-...More+
 Gas-assisted injection molding of kettle handlesWhat is the gas-assisted injection molding? Today we will talk about the case of gas-assisted injection molding of kettle handles. During the injection molding process, push the melt plastic to fi...More+
 Parallel barrel 2K injectionWhat is parallel barrel (2K) two-shot injection molding? What is 2K injection molding? Let’s see the what is called parallel barrel 2K injection molding. The injection molding machine used for...More+
 Pre-deformation MoldThe main reasons to cause the plastic parts are warpage and deformation1. The uneven wall thickness of each part of the plastic product deforms. Usually, the main part of the product is thicker and the ribs are thin, when the plastic parts are cooled.More+
 Video of Dongguan international machine tool exhibition in 2021USM (UNIQUE SOLUTIONS MOLD LIMITED) was founded in 2012 and is located in Dongguan City, Guangdong Province, a famous mould manufacturing province in China.More+
- Quality ControlQuality is the soul of USM at all times, the procedure of quality control, quality insurance, and quality monitoring are integrated into every operation step, and all operations are guaranteed with ISO 90001.More+
 Medical Pipette Tip MoldAs a medical plastic injection mold supplier, It has its own unique solutions from medical product development to mold design, mold manufacturing, and injection molding production.More+

- Insert pin of vengting design for molded partsInsert pin of venting:It is difficult to make exhaust slot when end runner is not in parting surface during injection, and there is no matching gap available, but we could make the venting pin at end ...More+
 Plastic injection mold runner system design pointsWhen designing the gating system, Firstly, we should consider making the plastic melt fill the cavity with core side quickly to reduce pressure and heat loss; secondly, it should be economically cons...More+
 What is 2K molding? What is L-shaped barrel two-color injection molding? What is 90-degree vertical barrel two-color injection molding?More+
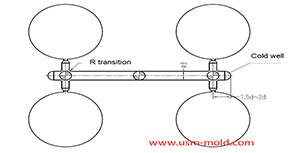 Key points of plastic injection mold runner systemThe sub-runner is a transitional channel between the main runner and the gate, as the sub-runner is the longgest part of gating system, so it is very important to enhance the parts quality and improve...More+
- PLC Controller Shell MoldMore and more people will have a high standard for a better life, most of home appliance product surfaces were made by mirror polishing, it requires for high standard to mold steel and polishing way, good mold steel without a technical polishing engineer, the product can not reach the high standard, they always work together.More+
- Slider of side core pulling mechanisum assemblingThe picture 1 shows a typical guide pin driven slider parting and core-pulling mechanism, we will talk about the composition and function of the lateral core-pulling mechanism.1. Lateral forming parts...More+
- Key points of plastic injection mold runner systemThe sub-runner is a transitional channel between the main runner and the gate, as the sub-runner is the longgest part of gating system, so it is very important to enhance the parts quality and improve...More+
- Video of Dongguan international machine tool exhibition in 2021USM (UNIQUE SOLUTIONS MOLD LIMITED) was founded in 2012 and is located in Dongguan City, Guangdong Province, a famous mould manufacturing province in China.More+
- USM Blogo OpeningHello everyone! Our blog is open today, it is very glad to have the opportunity to meet you here, welcome to visit us whenever you need.More+

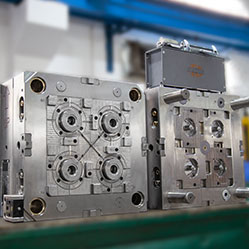 4 Cavity MoldA multi-cavity mold means that multiple identical parts are made in one set mold, and multiple identical parts can be produced in one injection cycle at the same time.More+
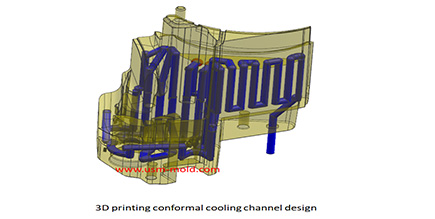 Design principle of plastic injection mold cooling systemDesign principle of cooling systemIn order to improve the efficiency of the cooling system and make the cavity surface temperature distribution even, the following principles should be followed in the...More+
 About UsUSM is one of the world's leading manufacturers of plastic injection mould and molded parts. We have always pushed developments forward and set benchmarks in Automtive, High precision and 2K moldi...More+
- Plastic Insert MoldThe easy formability and bendability of resin complement each other with the rigidity, strength, and heat resistance of the metal, and they can be made into complex and exquisite metal-plastic integrated products.More+
- Leading manufacturers of plastic injection mould and molded parts.We have always pushed developments forward and set benchmarks in Automtive, High precision and 2K molding and other industrial parts.More+
 Drip Tip MoldThe two-color molding will be made in one same injection machine at the same time by 2 times injection, with 2 injection barrels and 2 different injection gates by 2 different molds, but the product will be picked up one time, it will request 2 molds in one specific 2k injection machine to finish final injection.More+
- Design & EngineeringWe always insist that Design & Engineering is the core for mold, the USM engineering team will maintain communication closely with our customers at any time, from a project starting, they will participate in the customer's product design together.More+
- HomeEstablished in the year of 1996, HanKing start the business in mould making and injection molding in Longgang, Shenzhen, after years development, we have become a one-stop total plastic solution pr...More+
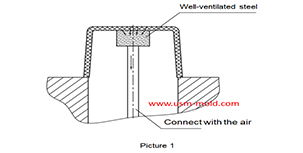 Well-ventilated steel of venting design for molded partsWell-ventilated steel is a sintered alloy, iIt is a porous material sintered with spherical particle alloys, the pore size is 7-10μm and the strength is poor, but the texture is loose which allow th...More+
- Pre-deformation MoldThe main reasons to cause the plastic parts are warpage and deformation1. The uneven wall thickness of each part of the plastic product deforms. Usually, the main part of the product is thicker and the ribs are thin, when the plastic parts are cooled.More+
- Engine Coolant PipeIn the gas-assisted injection molding process, the gas always follows the path with the least flow resistance, from high pressure to low pressure, and flows to the thick wall part, because the temperature of this part is high and the resistance is small.More+
- TV Frame MoldPushing the liquid plastic into the cavity and core side by high pressure during the injection process, and the gas pressure is maintained to form a hollow section inside the thick wall of the plastic part, the injection process is called gas-assisted injection molding.More+
- Insert pin of vengting design for molded partsInsert pin of venting:It is difficult to make exhaust slot when end runner is not in parting surface during injection, and there is no matching gap available, but we could make the venting pin at end ...More+
- Plastic cooling factors by injection parameter1. Plastic parts design: mainly for the wall thickness of plastic products. The thicker thickness of the product, the longer the cooling time. Generally speaking, the cooling time is approximately pro...More+
- Design principle of plastic injection mold cooling systemDesign principle of cooling systemIn order to improve the efficiency of the cooling system and make the cavity surface temperature distribution even, the following principles should be followed in the...More+
 Multi Cavities Hot Runner Injection MoldThe hot runner will keep the plastic material in liquid in runner and injection gate, the temperature in injection machine barrel and runner are very high which can keep the material in liquid, due to there is heating system surrounded, it will only need to heat the hot runner to request temperature before production, and the hot runner is like the extension of injection machine barrel.More+
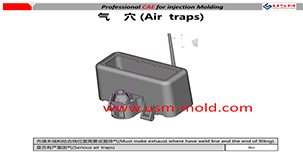 Reasons for making the exhaust system of the injection moldThe gas in the injection mold includes not only the air in the cavity, but also the air in the gate and the decomposition gas generated by the plastic melt, and the steam which caused by plastic in hi...More+
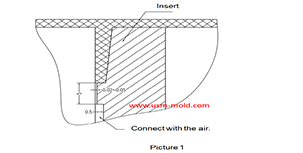 Venting insert design of molded partsIn the thin-walled cavity, the end of the melt flow, the bottom of the blind hole of the mold cavity, the end of the solid column of the plastic part, the bottom of the plastic part rib and screw colu...More+
- New Five-axis CNC Machine ArrivalThe new 5 axis CNC machining machine has arrived in our workshop on 6th Nov. 2021 and is now putting into use.GMU-6350 type CNC machining machineWorking stroke (XYZ): 630*500*550Maximum loading: 800kg...More+
- Venting system of plastic injection mold introductionHello everyone, thanks for attention. We’ve discussed about the temperature control system earlier, now we are going to talk about the mold venting information in following 11 articles, from the reas...More+
- Design & EngineeringWe always insist that Design & Engineering is the core for mold, the USM engineering team will maintain communication closely with our customers at any time, from a project starting, they will participate in the customer's product design together.More+
 Overmolding & 2k MoldingMaterial selection for two-color products: The same type of material of different colors is usually used for two-color injection molding so that the bonding strength of the first color and the second color plastic is the best.More+
- Visual Doorbell Housing MoldLighting control can adjust the lighting of all rooms by pressing a few buttons, the scene function can realize various scene modes, and the full turn on and off function can realize the one-key to turn on and off functions of all lamps and lanterns.More+
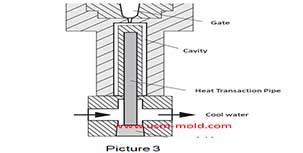 Plastic injection mold common cooling gate1. Straight-through cooling water gate: the straight-through cooling gate is the most commonly used gate for plastic injection mold, and it is also the most convenient type of cooling for processing. ...More+
- 2022 Shenzhen Industrial Exhibition ITES ended successfullyThe 2022 ITES Shenzhen International Industrial Manufacturing Technology and Equipment Exhibition and the 23rd Shenzhen International Machinery Manufacturing Exhibition were grandly opened in Shenzhen...More+

 Water Assisted Injection MouldBecause the flow rate of the outer layer of the melt is slow and the speed of the inner layer is fast, the inner layer of melt will roll outwards and stick to the mold cavity while advancing.More+
- Air Chamber MoldWith over 15 years of pre-deformed mold, USM Mold has mastered scientific and complete pre-deformation mold technology, from project management, mold flow analysis, design, manufacturing, assembling, mold trial, and final measurement.More+
- Pre-deformation MoldThe main reasons to cause the plastic parts are warpage and deformation1. The uneven wall thickness of each part of the plastic product deforms. Usually, the main part of the product is thicker and the ribs are thin, when the plastic parts are cooled.More+
- Multi Cavities Hot Runner Injection MoldThe hot runner will keep the plastic material in liquid in runner and injection gate, the temperature in injection machine barrel and runner are very high which can keep the material in liquid, due to there is heating system surrounded, it will only need to heat the hot runner to request temperature before production, and the hot runner is like the extension of injection machine barrel.More+
- Five Major Steps of the Injection Mold Production ProcessInjection mold manufacturing can be roughly divided into the following steps:Process analysis of plastic products.More+
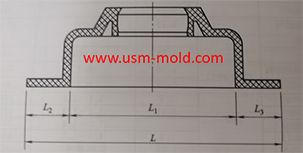 Plastic molding shrinkage ratePlastic parts getting smaller by shrink, due to the temperature decrease during the molding process, and the shrinkage is expressed by the shrinkage rate, it is common plastic shrinkage rates are show...More+

- The basic points of designing gas-assisted injection molding1. Firstly, considering the suitable wall thickness areas needs to be injected and hollowed out, and then decide how to connect them with the gas channel;2. The gas channel should be arranged in balan...More+
- Slider designing tips 11. After the slider core pulls out, the length of staying in the guide pin slot should not be less than 2/3 of the total length of the slider, for special cases, the slider slot can be partially lengt...More+
 Automotive Water Intake Manifold MouldGas injection methods can be divided into two types, one is to inject gas together with the melt through the machine nozzle, and the other is to directly inject gas into the runner or cavity through the gas injection element (gas needle), the latter is divided into single-point intake and multi-point intake.More+
- Venting insert design of molded partsIn the thin-walled cavity, the end of the melt flow, the bottom of the blind hole of the mold cavity, the end of the solid column of the plastic part, the bottom of the plastic part rib and screw colu...More+
 Dongguan International Machine Tool Exhibition of 2021 hedling successfully2021 is an extraordinary year, although the epidemic has not completely subsided, it cannot stop the enthusiastic pursuit of new equipment and new technologies in the Chinese manufacturing industry.More+
 Video of CNC Machining Processing by Dongguan International Machine Tool Exhibition in 2021The 3rd China Machine Tool Purchasing Festival-DME Dongguan International Machine Tool Exhibition (hereinafter referred to as DME) was grandly closed at Guangdong Modern International Exhibition Center (Dongguan Houjie) on 13th Dec. 2021.More+
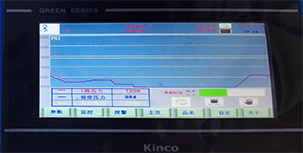 Key points of gas-assisted injection molding processGas injection parametersThe gas-assisted control part is a device that controls the gas pressure in each stage, the gas-assisted parameters have only two values: gas injection time (seconds) and gas i...More+
- The principle of mold temperature balance in plastic mold cooling system designThe principle of mold temperature balance:1. Due to the complexity of the plastic parts and mold structure, it is difficult to make the temperature of the mold completely consistent, but should be mak...More+
 The T slot of slider and guider designing tips1. The T slot of slot should be designed according to the picture 1, If there is a relatively high slider, the slider T slot is not high enough which will ...More+
- Design principle of plastic injection mold cooling systemDesign principle of cooling systemIn order to improve the efficiency of the cooling system and make the cavity surface temperature distribution even, the following principles should be followed in the...More+
- Reasons for making the exhaust system of the injection moldThe gas in the injection mold includes not only the air in the cavity, but also the air in the gate and the decomposition gas generated by the plastic melt, and the steam which caused by plastic in hi...More+
- Automotive Mold SupplierWith over 15 years of experience in automotive mold development and production, USM will make mold flow analysis from the DFM report step to ensure that the pressure will be controlled at a reasonable range during injection, and there are no weld marks and other defects on the part surface.More+
 3 Precision Molds Are Ready to Ship GermanyAfter 2 months later, the 3 molds have been finished and ready to ship. From DFM report to mold design to manufacturing and T1 samples were provided in 6 weeks.More+
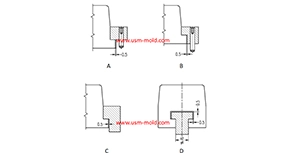
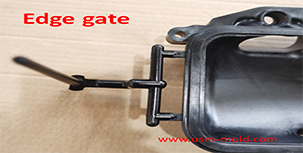 Side gate of plastic injection mold runner system designIn order to get the best injection quality, the gate type must be selected carefully, the coommon gate tyeps are: direct gate, side gate, pin-point gate, sub gate,valve gate of hot runner etc. Among...More+
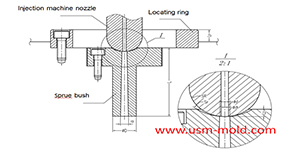 The main design points of the design of the plastic mold pouring systemThe main runner is the part where the molten plastic first passes when it is sprayed from the injection nozzle, and it is coaxial with the injection nozzle, because of repeated contact and collision w...More+
- Well-ventilated steel of venting design for molded partsWell-ventilated steel is a sintered alloy, iIt is a porous material sintered with spherical particle alloys, the pore size is 7-10μm and the strength is poor, but the texture is loose which allow th...More+

- Hydraulic diameter conversion of runners in plastic mold gating system designHydraulic diameter refers to 4 times the ratio of the flow cross-sectional area to the perimeter, as the wall shear stress of non-circular pipes is not even distributed along the surrounding walls, on...More+
 Medical TPE MoldSince the establishment of the factory, USM has provided injection molding products and injection mold services for many medical companies around the world, especially in medical multi-cavity and small products (pipetting tips) with rich and valuable experience.More+
- The common fixing method of angle pinThe angle pin is a common part of the drive slider, and the fixing and installation methods as following:1. Pass through the mold plate directly and press the angle pin with the top plate to fix it, a...More+
 Plastic part ribs desiginingThe ribs function: The role of ribs is to improve the strength and rigidity of the plastic parts, prevent the plastic parts from being distorted and deformed, and will not cause the appearance of t...More+
- Metal Insert MoldFor rigid molded parts and curved elastic molded products on rubber gaskets, after injection molding on the substrate, an integrated product can be made, and the complicated operation of arranging the sealing ring can be omitted, making the automatic combination of the subsequent processes easier. Because it is the joining of the molten material and the metal insert, compared with the press-in molding method, the gap of the metal insert can be designed to be narrower, and the reliability of composite product molding is higher.More+
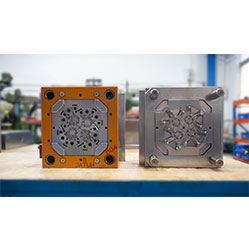 Insert Mold PartsInsert molding is injected with plastic part processing, the insert can be plastic or metal, normally it will be metal parts or thread parts, they must be in a fixed area before injection, so it will be fitting very well after injection finishing. Normally these products request a high standard of strength.More+
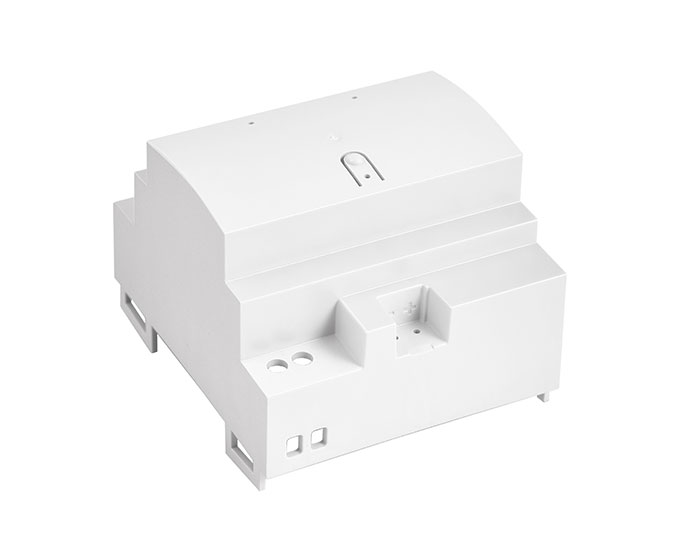 Plastic Household MouldAdvantages of Smart Home Appliance MoldMeet different demandsIn order to meet the different types of demands, grades, and styles, the control host of the smart home system can also be upgraded online.More+
- What is the side parting and core pulling mechanisms with their function?When there are holes, cavities or cores on the inside or outside of the injection-molded plastic parts that are different from the opening and closing directions of the mold, the plastic parts cannot...More+
- Parting surface venting of runner systemThere are a large amount of gas in the main and sub channel, these gas are discharged through the pull rod (push rod) during injection processing, a part of gas come out from exhaust slot on parting s...More+
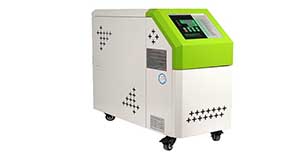 Plastic injection mold heatingWhen the plastic injection molding process requires the mold temperature to be above 80°C, a temperature adjustment system with heating function must be provided in the mold. In addition, thermoplast...More+
- Overmolding & 2k MoldingMaterial selection for two-color products: The same type of material of different colors is usually used for two-color injection molding so that the bonding strength of the first color and the second color plastic is the best.More+
- Medical Plastic MoldProduct material: PP material in medical-gradeMold steel: S136 HRC 52-54Mold life: 1 millionHot runner brand: IncoeMold base: LKMSurface finishing: Mirror polishingMold lead time: 6 weeksMore+
- HomeEstablished in the year of 1996, HanKing start the business in mould making and injection molding in Longgang, Shenzhen, after years development, we have become a one-stop total plastic solution pr...More+
- Medical Plastic Injection MoldWhat is the medical injection molded parts?For medical plastic manufacturers, it means that medical supervisors are required to supervise and manage the materials used to manufacture the equipment.More+
- Transparent PC Injection MoldType-J thermocouple, the positive electrode of this thermocouple is pure iron, and the negative electrode is constant (copper-nickel alloy).More+
- The basic points of designing gas-assisted injection molding1. Firstly, considering the suitable wall thickness areas needs to be injected and hollowed out, and then decide how to connect them with the gas channel;2. The gas channel should be arranged in balan...More+